Bulk Material Handling Applications in Chemical Handling
From powder to granule — precise, safe, and contamination-free chemical handling.
Recommended Equipment for Chemicals
From fertilizers and pigments to detergents, catalysts, and specialty chemical powders, chemical handling demands the highest standards of purity, safety, and precision. Even trace contamination or moisture ingress can compromise product quality, while dust emissions pose health and safety risks. Our bulk handling equipment is engineered for the rigorous demands of chemical processing — with sanitary stainless steel or coated construction, inert gas purging options, dust-tight sealing, and ATEX-compliant designs for explosive environments. Whether you’re handling fine powders, hygroscopic granules, or corrosive materials, our solutions keep your chemicals pure, safe, and moving reliably from production to packaging to dispatch.
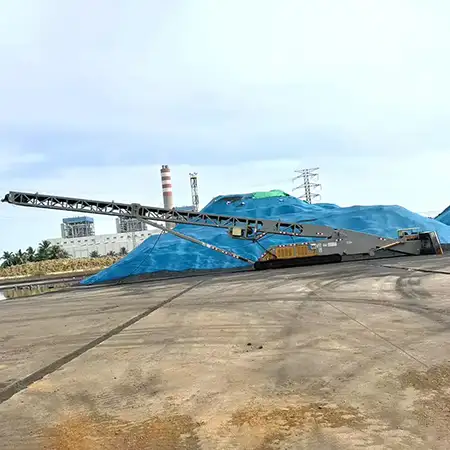
This mobile conveyor handles chemical powders and granules with exceptional care. Its smooth, gentle conveying action minimizes degradation and fines generation, while the enclosed, dust-tight design prevents contamination and moisture ingress. Sanitary construction options are available for food-grade and pharmaceutical chemicals.
Built for chemicals:
Gentle conveying action — minimizes product degradation Dust-tight enclosure — prevents contamination and moisture ingress
Sanitary construction options — for food-grade and pharma applications Mobile crawler chassis — flexible plant access
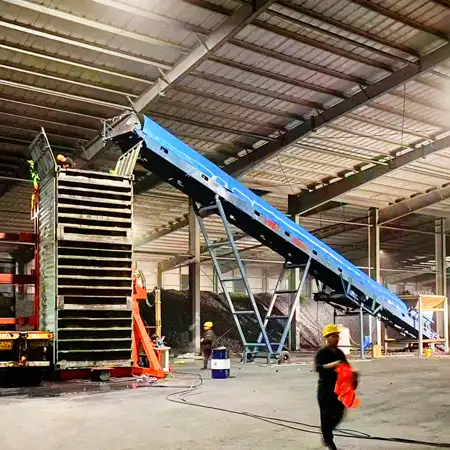
This container tilter enables clean, dust-free loading and unloading of chemical materials into shipping containers. Its enclosed, gas-tight design prevents contamination and moisture exposure, while gentle rotation minimizes product degradation. Compatible with container liners and available in stainless steel construction for corrosive or high-purity chemicals.
Built for chemicals:
Container liner compatibility — contamination-free transfer Dust-tight, gas-tight enclosure — protects sensitive chemicals
Gentle rotation control — prevents product degradation Stainless steel options — for corrosive or high-purity materials
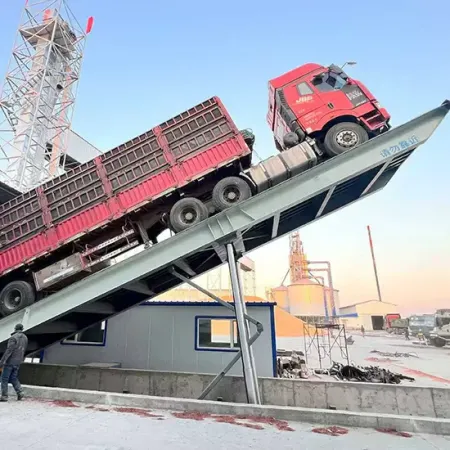
This hydraulic truck unloading platform provides fast, clean transfer of chemical materials from trucks to silos or processing lines. Its enclosed transfer points and integrated dust collection system ensure emission-free operation, while controlled lifting angles prevent material degradation and spillage.
Built for chemicals:
Enclosed transfer points — emission-free operation Controlled lifting angle — prevents degradation and spillage
PLC-synchronized cylinders — stable, reliable lifting ATEX-compliant options — for explosive chemical environments
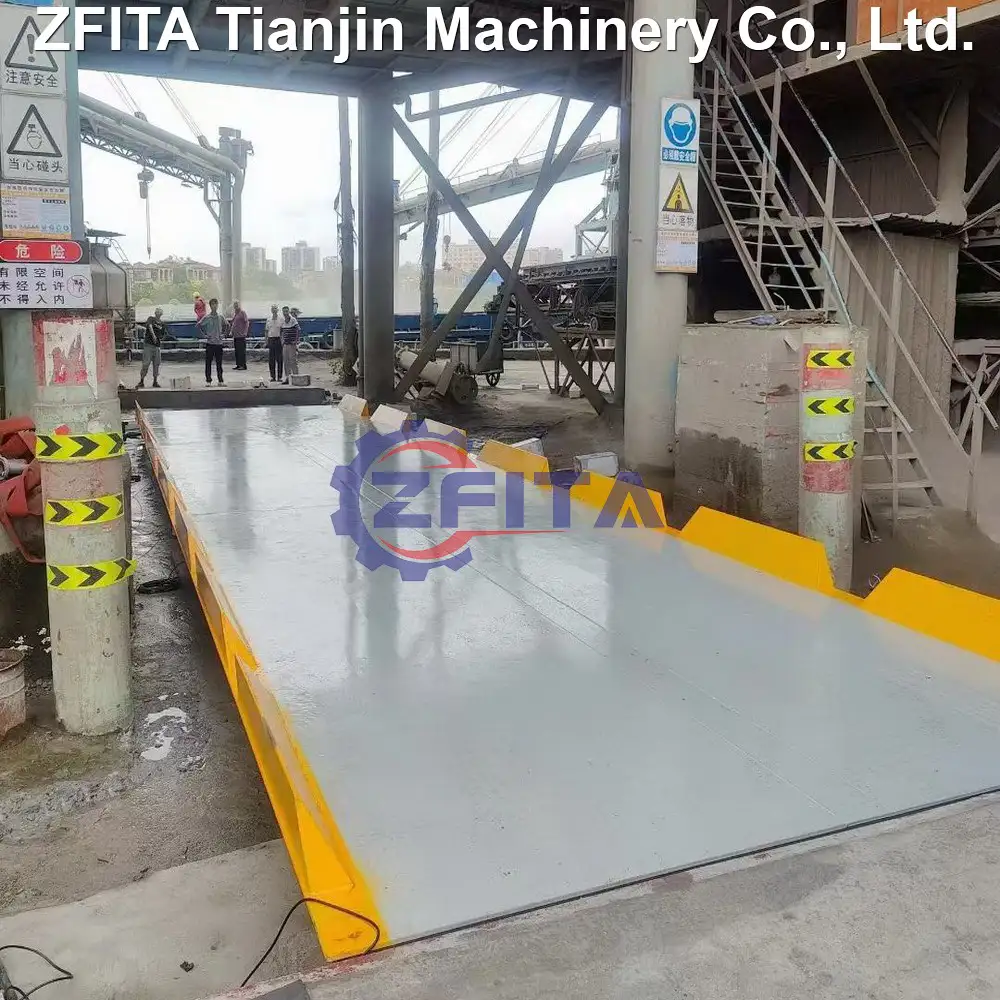
This precision truck scale delivers accurate, reliable weighing for incoming raw chemical shipments and outgoing finished products. Its rugged construction and corrosion-resistant finish withstand the harsh conditions of chemical plants, while optional software integration enables seamless data capture for inventory management and quality compliance.
Built for chemicals:
High-precision weighing — accurate inventory and compliance tracking Corrosion-resistant construction — withstands chemical exposure
Rugged steel deck — handles heavy truck traffic Optional data integration — seamless record keeping
Suggested Solutions
Industry Challenges Limited Container Space Utilization Traditional horizontal loading methods
Industry Challenges Inefficient Bulk Loading with Traditional Bagged Methods Many
Industry Challenges High Labor Dependency Manual unloading is costly and
Book a video meeting with our engineers →
Discuss your material handling requirements directly with our engineers. We will help you evaluate the right equipment solution based on your application, capacity, and site conditions.
Request a Quote
Tell us your material handling requirements. Our engineering team will provide a customized solution and quotation.